
Rapid Tooling vs Vacuum Casting — Enclosure RFQ China
When vacuum casting: geometry still moving, colour-matched urethane or soft-touch covers / housings, about 10 to a few thousand without an injection tool (RIM for larger shells). When rapid tooling: design frozen, need production thermoplastic grades and molded repeatability at bridge volume (aluminum soft tools, T0–T3). Upload STEP on /contact for one Suzhou enclosure RFQ — usually within one working day.
Why buyers compare rapid tooling and vacuum casting
Overseas buyers often ask when a cover should stay on urethane casting and when it should move onto a rapid aluminum injection tool. The two routes fail on opposite constraints: casting skips hard tooling; rapid tooling buys molded resin repeatability once geometry is frozen.
Everoyal runs vacuum casting and RIM beside rapid tooling (aluminum and steel molds, T0–T3 on site) at one Suzhou base (est. 2017; ~10,000 m²; ~80 staff; 50+ machines), with CNC, sheet metal and 3D printing under the same contract. Process RFQ landings: rapid tooling China · vacuum casting China · 3D printing China. Programs: robotics · services hub · more compares: compare hub. Sister compares and guides: CNC machining vs rapid tooling, 3D printing vs vacuum casting, vacuum casting vs CNC, vacuum casting vs injection moulding, MOQ prototype & small batch. This page is the enclosure / cover cast-vs-soft-tool decision guide — not a price list. RFQ → /contact.
Vacuum casting / RIM
CNC master → silicone mold → urethane pour. Soft or hard resins, colour-tunable covers; RIM for larger enclosures. About 10 to a few thousand without steel tooling.
Rapid tooling (T0–T3)
Aluminum soft tools (and trial steel when volume justifies). Tool cut, T0 first shot through T3 sign-off, then molded thermoplastic small batches at the same base.
Bridge path
Cast while geometry moves; cut rapid tooling from the same approved data once resin grade and volume need molds — one vendor, one crate from Suzhou.
Rapid tooling vs vacuum casting — what changes for RFQ buyers
| Factor | Vacuum casting / urethane (RIM) | Rapid tooling (aluminum / steel, T0–T3) |
|---|---|---|
| What it is | Resin poured under vacuum into a silicone mold from a CNC master | Injection into a cut aluminum (or trial steel) mold; documented T0–T3 trials |
| Tooling need | CNC master + silicone mold (remade when copy count ends); RIM soft epoxy/aluminum tooling for larger shells | Aluminum soft tool or trial steel mold; cavity count set by batch/annual volume |
| Lead-time band | Master + mold setup before first pour; then batch copies. Timing depends on polish, colour and qty — see prototype lead times; no invented day counts here | Rapid aluminum tooling typically planned ~2–3 weeks at Suzhou with T0–T3 before batch; trial steel ~4–6 weeks; production steel longer — geometry must be frozen. Context: lead-times page |
| Cosmetics / colour | Production-like urethane surfaces; soft/hard resins colour-tunable to sample or Pantone | Molded thermoplastic surfaces; texture and colour from tool/resin grade and secondary finish |
| Material options | Soft or hard urethane resins (and RIM compounds) — casting grades, not always identical to production injection plastics | Production thermoplastic grades (fillers noted on RFQ); tool steel grade extends life when volume is confirmed |
| Quantity bands | ~10 to a few thousand; silicone mold limited copy count. MOQ guide: MOQ prototype & small batch | Bridge when roughly a thousand to a few thousand molded parts pay for the tool before steel; aluminum tool life often planned ~1,000–5,000 shots (planning range, quote states duty) |
| Tolerance / fit | Cast surface for cosmetics; tight interfaces still need CNC or secondary machine work | Molded dimensions measured at T1–T3; shrinkage from this tool’s data; mating faces can still be secondary-machined |
| Typical use | Cosmetic covers, robot enclosures, soft-touch shells while design is still moving | Frozen geometry needing molded resin repeatability and thermoplastic grades at bridge volume |
| Common RFQ miss | Staying on casting after geometry and volume already justify a soft tool | Cutting aluminum while design is still changing (expensive rework vs remaking a silicone mold) |
| When to prefer | Colour-matched urethane / soft-touch at tens–thousands without injection tools | Frozen design + molded thermoplastic + volume/repeatability that pays for T0–T3 |
Service overviews: rapid tooling & molding, vacuum casting & RIM. China RFQs: rapid tooling China, vacuum casting China. Exact lead times, shot life and resin grades are agreed in the quote from your drawing — not published as certified catalog defaults. No invented ISO / customer / medical / die-casting claims on this page.
Cast and soft-tool under one China contract
Vacuum casting China RFQ
Urethane casting and RIM from CNC masters — soft/hard resins, colour sample, batch band. Vacuum casting China.
Rapid tooling China RFQ
Aluminum and steel molds, T0–T3 on site, trial molding beside the tool. Rapid tooling China.
Sister compares
CNC vs soft tool: CNC machining vs rapid tooling. Print vs cast: 3D printing vs vacuum casting. Cast vs CNC: vacuum casting vs CNC. Print China RFQ: 3D printing China. Programs: robotics · services · compare.
Bridge path
Keep masters and cast shells while geometry moves; cut rapid tooling from the same approved STEP once volume and resin grade justify molds.
Lead-time honesty
Qualitative bands only on this page (aluminum ~2–3 weeks planning band from site lead-times). Exact dates come with the quotation. Context: prototype lead times.
Honest limits
No catalog prices, shot-life guarantees or resin certificates without your drawing. Quote depends on geometry, material family, quantity and finish notes.
What to send when choosing cast vs soft tooling
You can ask for both process options on one STEP pack. Quantity band, geometry freeze status and material family still come first.
| Item | Preferred | If missing |
|---|---|---|
| 3D + critical 2D | STEP / IGES + PDF with cosmetic faces and parting notes | Mold split / gate guessed |
| Process preference | Vacuum cast / RIM or rapid aluminum/steel tool — or “quote both / bridge path” | Quoted default may not match duty |
| Material / resin | Urethane Shore or hardness; or thermoplastic grade + fillers for tooling | Material stays a range |
| Colour / cosmetics | Sample, Pantone, texture notes | Colour match re-quoted after first article |
| Qty / Incoterm | 10 / 50 / 200 / 1,000+; FOB / CIF / DDP; say if geometry is frozen | Lead time and tool type stay a range |
| Fit-critical faces | Which bores / pads need post-machine after cast or mold | Fit stays on cast or molded tolerance |
Upload on /contact (2 files × 4 MB). Packing list: RFQ checklist. Quantity bands: MOQ prototype & small batch. Factory facts: Everoyal at a glance.
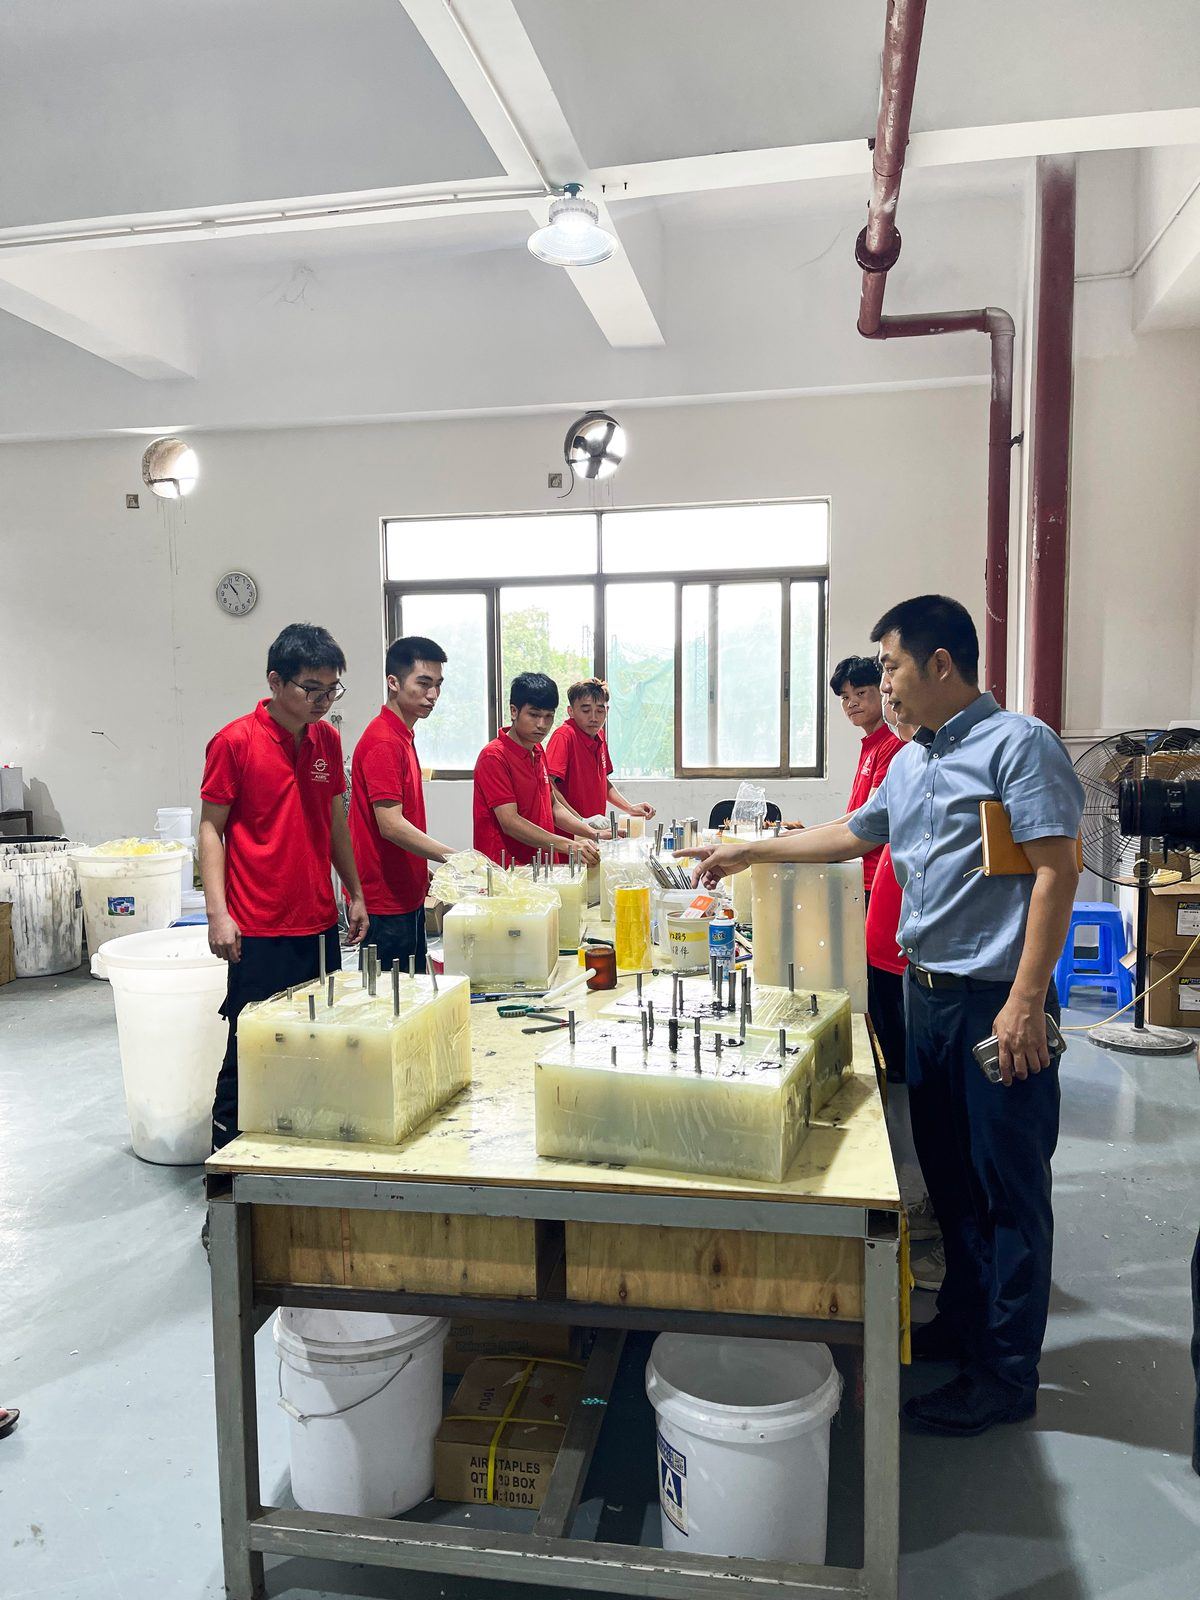 Vacuum casting workshop
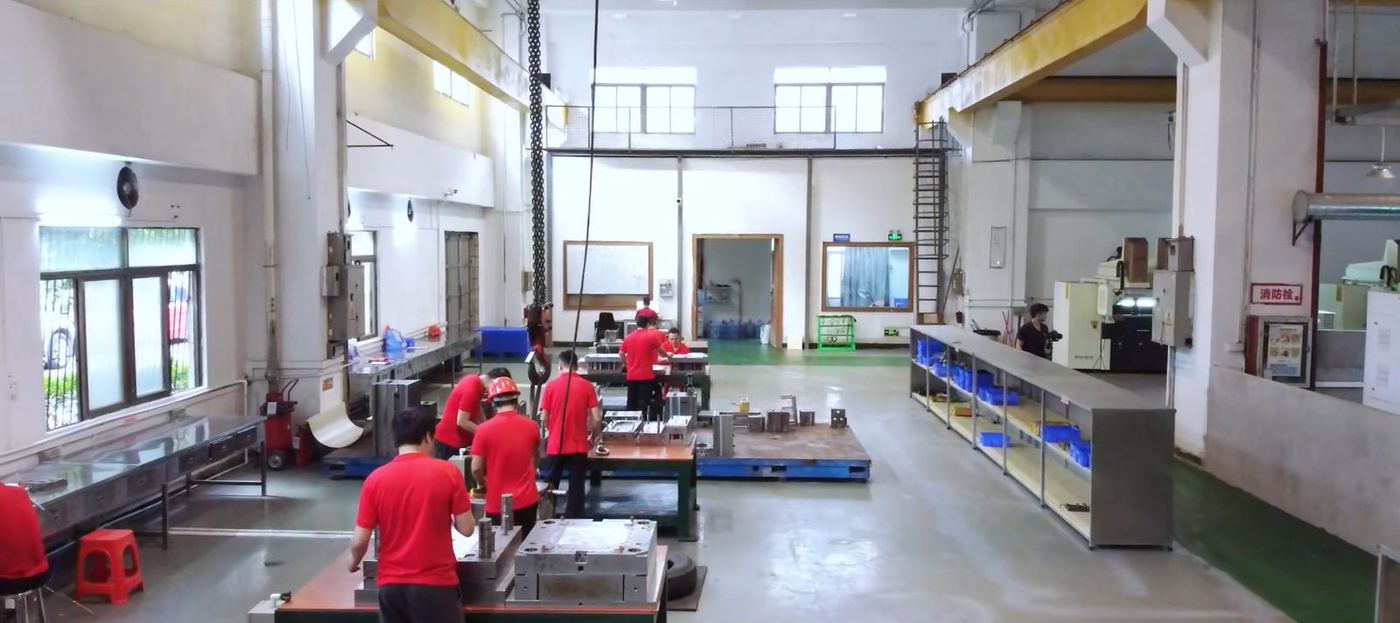 Rapid tooling workshop
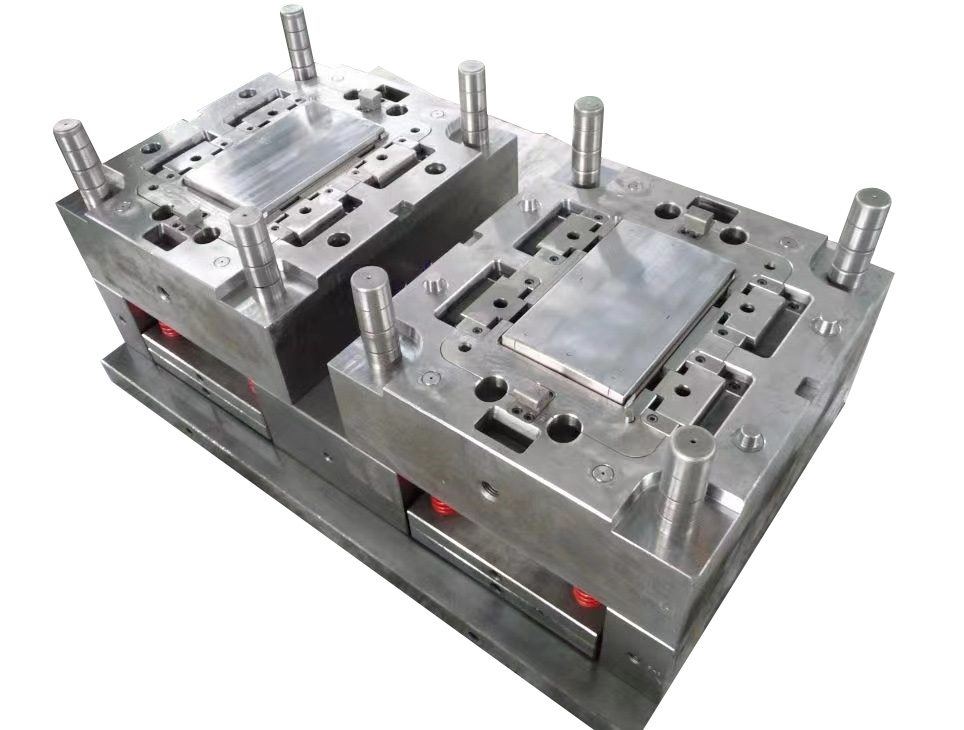 Multi-cavity rapid tool
Fast rules that keep cast vs soft-tool quotes comparable
Geometry still moving → cast
Silicone remakes cost less than aluminum rework. Prefer vacuum casting / RIM for colour and soft-touch at tens–thousands.
Frozen + molded resin → rapid tool
Call aluminum soft tooling with T0–T3 when thermoplastic grade and volume/repeatability need molds.
One crate from China
Cast covers and molded bridge parts under one FOB / CIF / DDP quote. Facts: Everoyal at a glance.
When should I choose rapid tooling vs vacuum casting for an enclosure RFQ?
Choose vacuum casting (and RIM for larger shells) while geometry is still moving, for colour-matched urethane or soft-touch covers / housings at about 10 to a few thousand without an injection tool. Choose rapid aluminum tooling (T0–T3) when the design is frozen and you need production thermoplastic grades plus molded repeatability at bridge volume. Upload STEP on /contact for a Suzhou quote of either or a bridge path. Sister RFQs: rapid tooling China, vacuum casting China, 3D printing China.
What is the difference between rapid tooling and vacuum casting for covers?
Vacuum casting pours urethane into a silicone mold taken from a CNC master — soft tooling for cosmetic or soft-touch covers without injection. Rapid tooling cuts an aluminum (or trial steel) injection mold, runs T0–T3 trials on site, and molds thermoplastic parts. Casting wins while geometry is still moving and volume stays in the tens to low thousands of urethane parts; rapid tooling pays once geometry is frozen and you need molded resin repeatability.
When should I choose vacuum casting over rapid tooling?
Prefer vacuum casting (and RIM for larger enclosures) for colour-matched urethane covers, soft-touch housings, and batches of about 10 to a few thousand without cutting an injection tool. Prefer rapid aluminum tooling when the design is frozen, you need production thermoplastic grades, and quantity or repeatability makes a soft mold pay — typically bridge volumes before full steel. Exact break-even depends on cycle time and tool cost, confirmed in the quote. Quantity framing: MOQ prototype & small batch.
What tooling does each process need?
Vacuum casting needs a CNC master pattern and a silicone mold (remade from the same master when copy count ends); RIM uses soft epoxy/aluminum tooling for larger shells. Rapid tooling needs an aluminum soft tool or trial steel mold, with T0 first shot through T3 sign-off documented at the same Suzhou base before batch release. Sister path: vacuum casting vs injection moulding.
What quantity bands fit vacuum casting vs rapid tooling?
Vacuum casting and RIM typically bridge about 10 parts to a few thousand cosmetic or soft-touch pieces; a silicone mold has a limited copy count. Rapid aluminum tooling is planned when you need roughly a thousand to a few thousand molded thermoplastic parts before steel is justified — typical aluminum tool life is on the order of 1,000 to 5,000 shots depending on resin and gate wear (planning range, not a guarantee). Timing context: prototype lead times.
Can a program move from vacuum casting to rapid tooling at Everoyal?
Yes. That is the intended bridge: cast covers while geometry moves, then cut rapid aluminum tooling from the same approved data once volume and resin grade justify molds. Vacuum casting, RIM, rapid tooling T0–T3, CNC and sheet metal share one Suzhou base (est. 2017; ~10,000 m²; ~80 staff; 50+ machines), so the vendor does not change. Upload STEP on /contact (up to 2 files, 4 MB each).
Can Everoyal quote rapid tooling and vacuum casting in the same China order?
Yes. Tool design, cutting, T0–T3 and small-batch molding sit beside vacuum casting and RIM at the Suzhou base. Upload STEP or IGES and a PDF on /contact (up to 2 files, 4 MB each) with process preference, material or resin grade, quantity and Incoterm. Sister RFQs: rapid tooling China, vacuum casting China. Reply is usually within one China working day.
Also useful: rapid tooling China, vacuum casting China, 3D printing China, robotics, services, compare hub, CNC vs rapid tooling, 3D printing vs vacuum casting, vacuum casting vs CNC, MOQ, contact.
Upload STEP for an enclosure cast vs soft-tool RFQ
Attach STEP, IGES or PDF on /contact (up to 2 files, 4 MB each). Note cast vs rapid tooling preference, material, colour and quantity. Rocky Chen replies with process options, DFM risks and a quotation — usually within one working day.