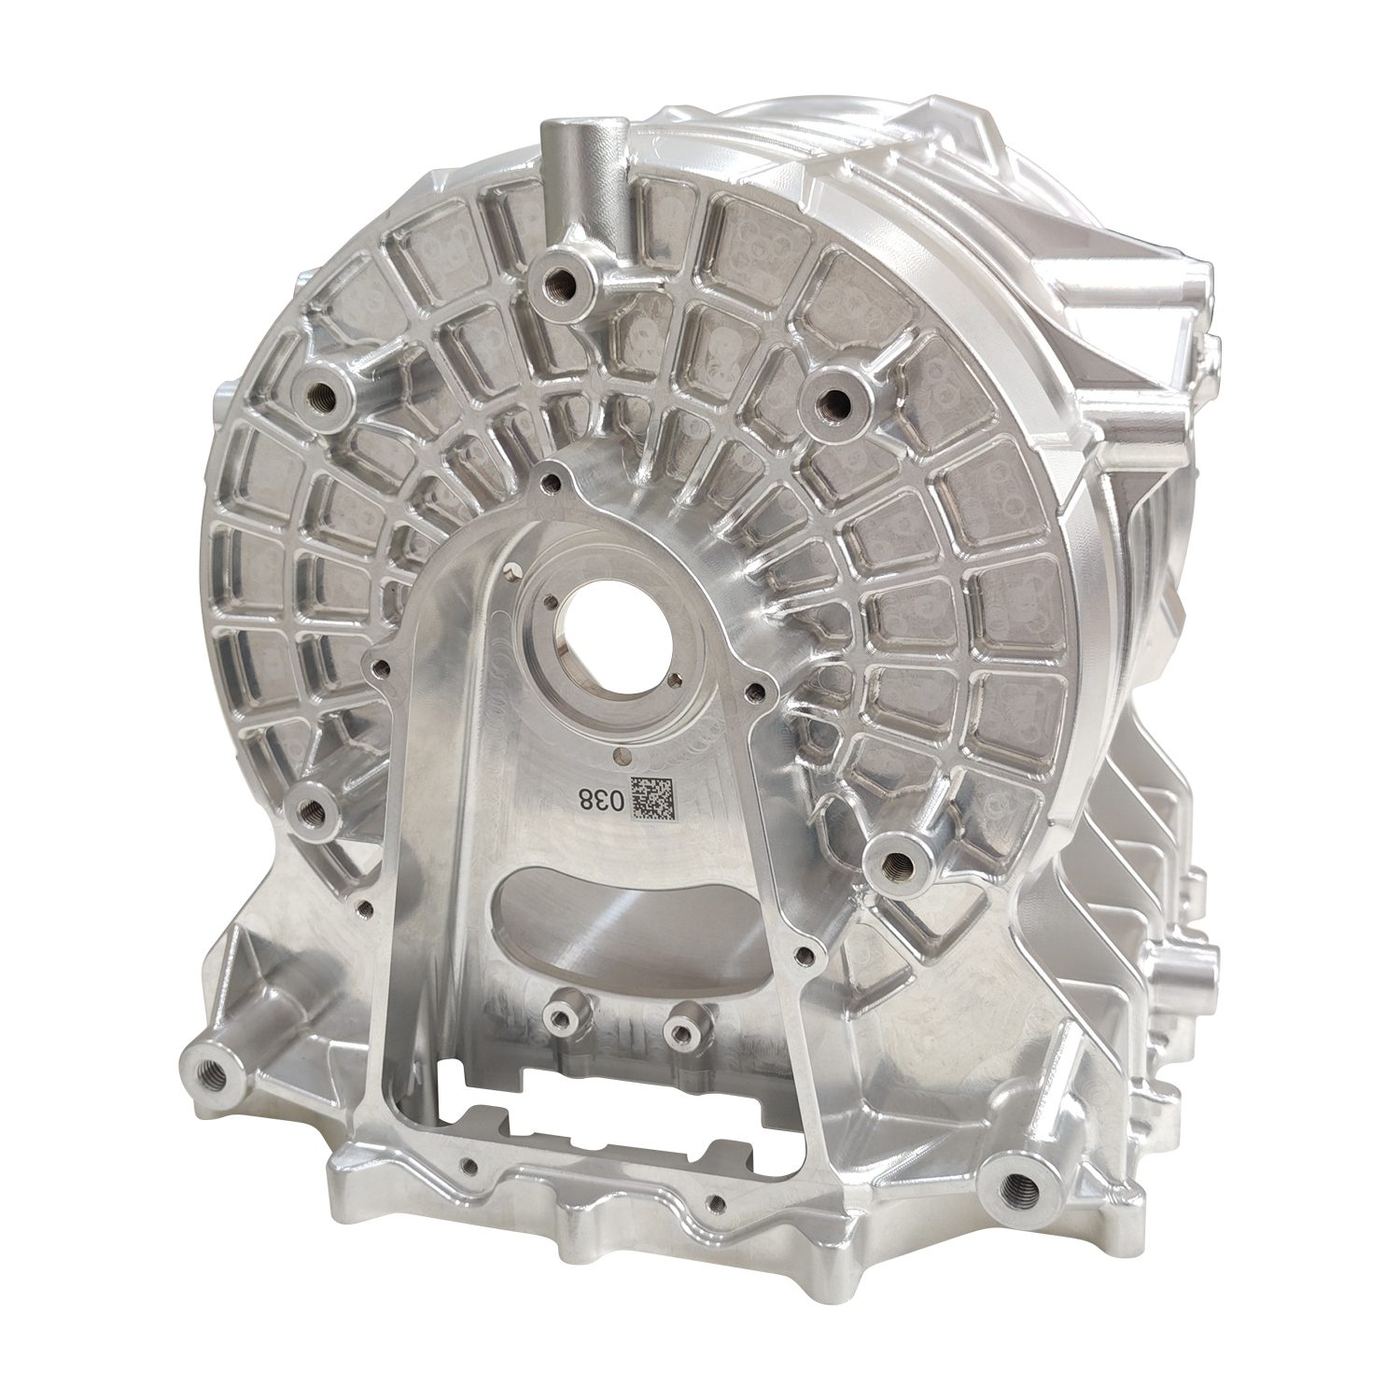
CNC machining & turning-milling
Aluminium, stainless and engineering-plastic parts, shafts and joint housings, plus a five-axis gantry for large frames.
Bore 0.01 mm35,000 rpm
Six processes, one contract, one shipment. A robot programme usually needs machined aluminium, cast cosmetic covers, printed internal brackets and a welded frame at the same time.
Aluminium, stainless and engineering-plastic parts, shafts and joint housings, plus a five-axis gantry for large frames.
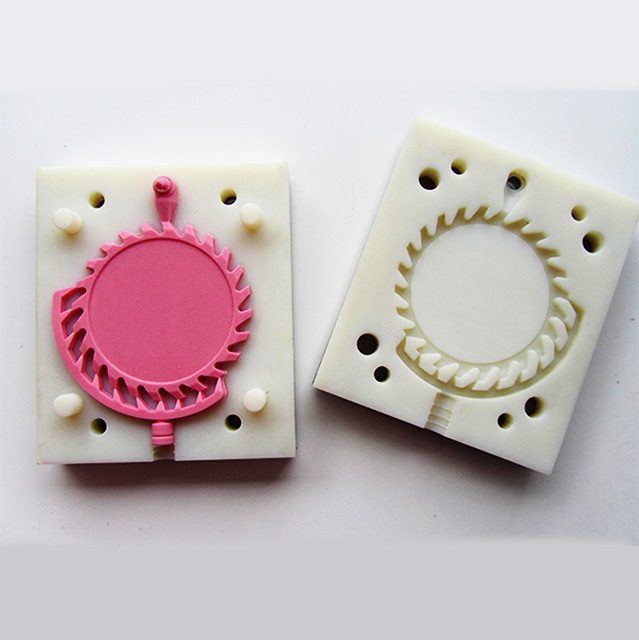
Silicone-mould casting off a machined master in tunable colour, soft or hard resin. RIM for larger enclosures.
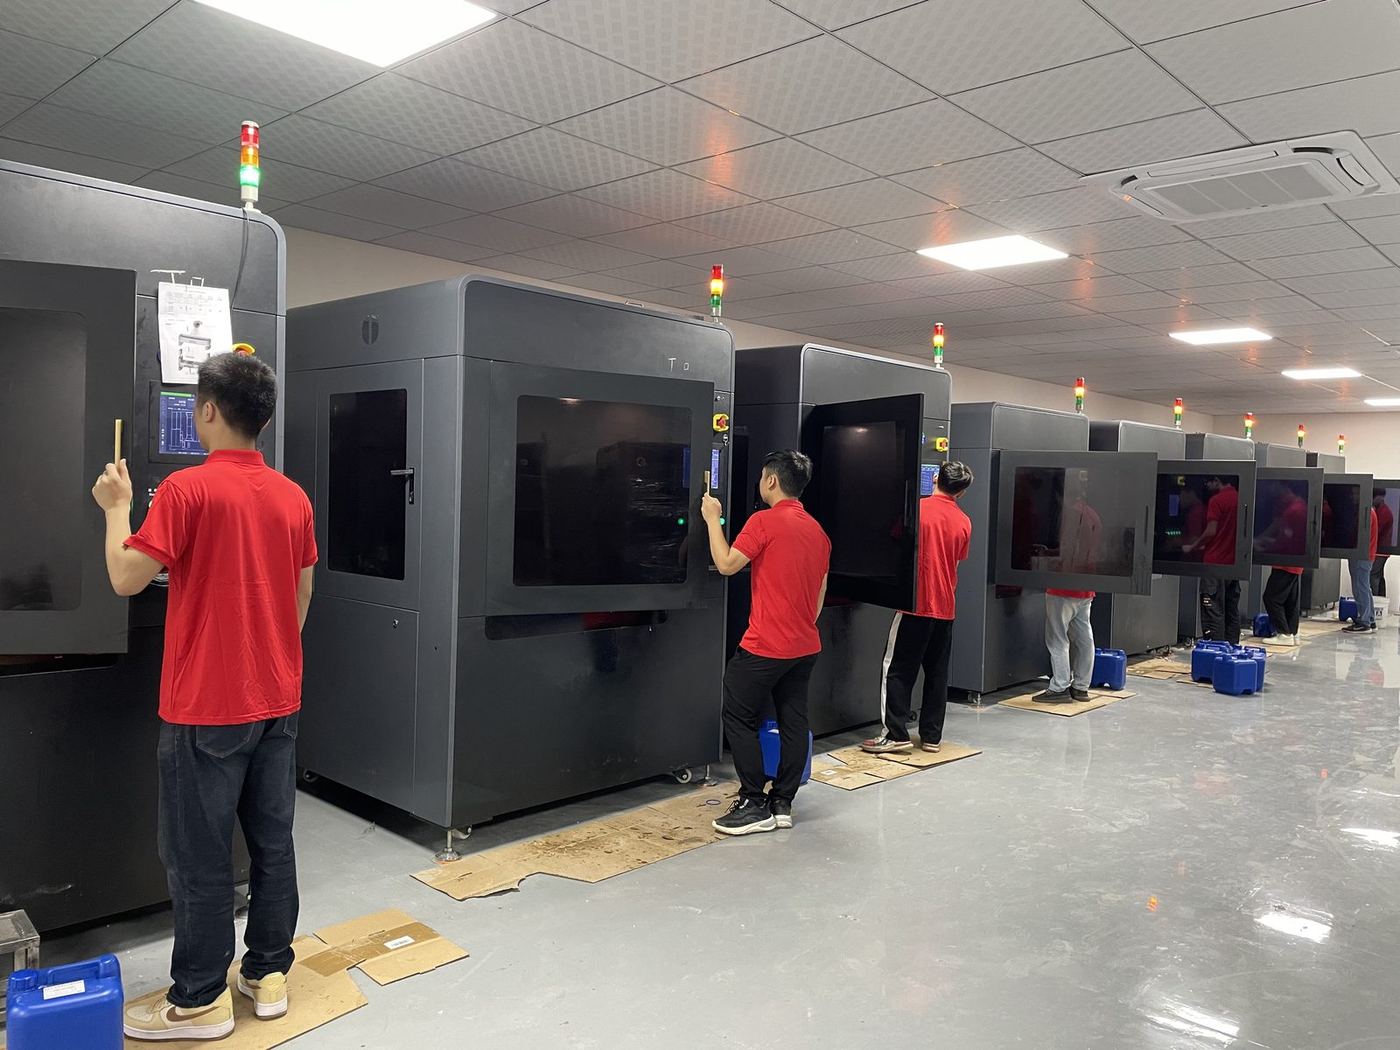
Internal brackets, lattice structures and one-off functional parts, printed, finished and coloured at the same base.
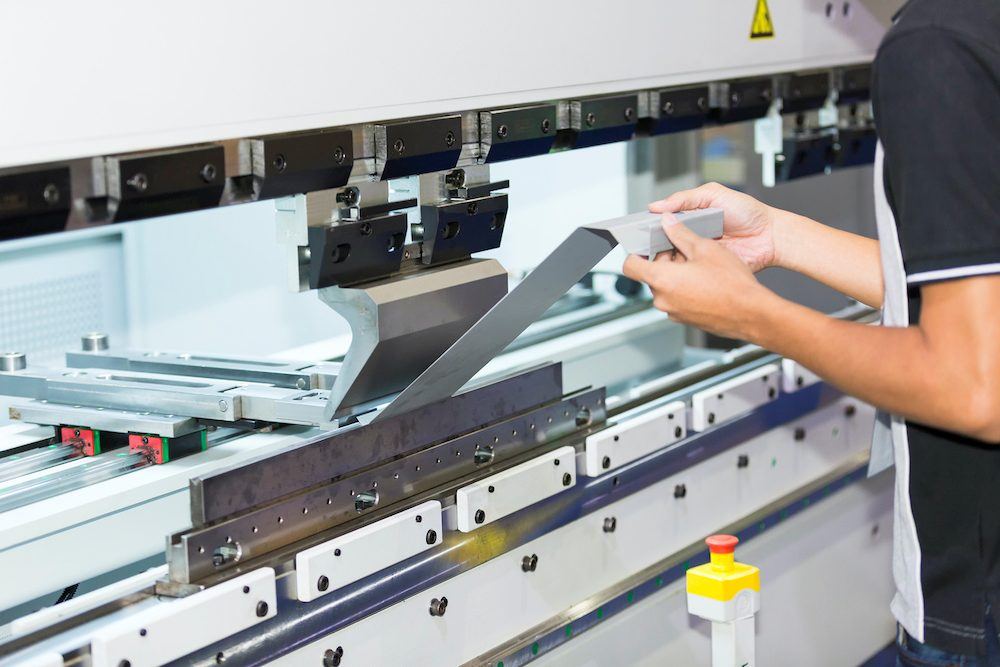
Frames, panels and battery enclosures: laser cutting, punching, CNC bending, welding, hand finishing.
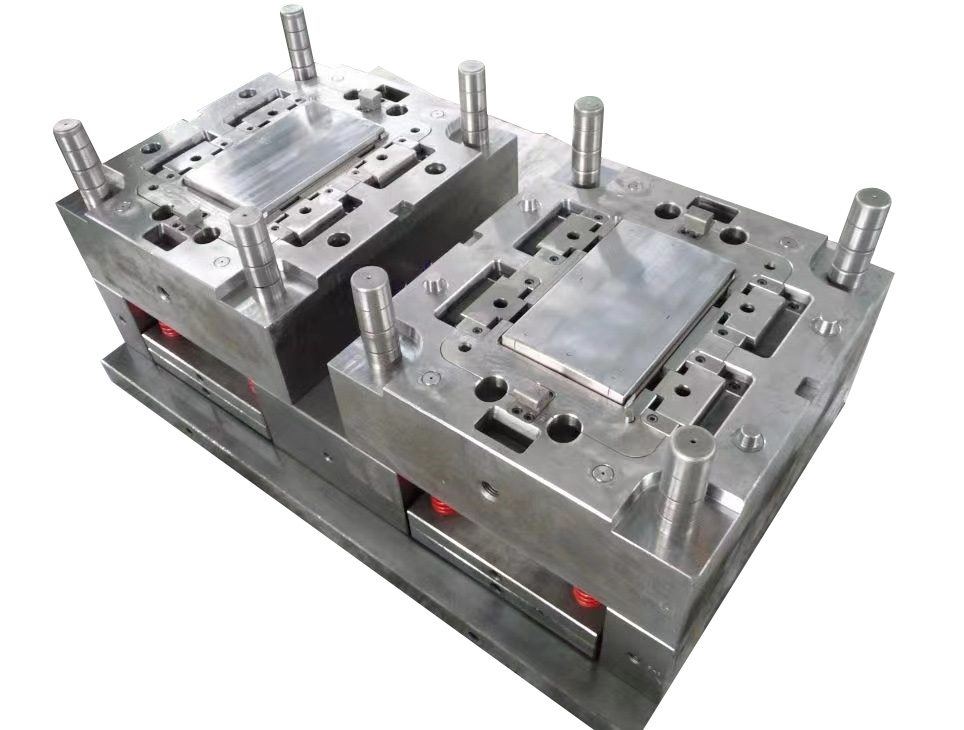
Rapid aluminium and steel moulds, DFM and mould-flow review, T0 to T3 sampling, trial and small-batch moulding.
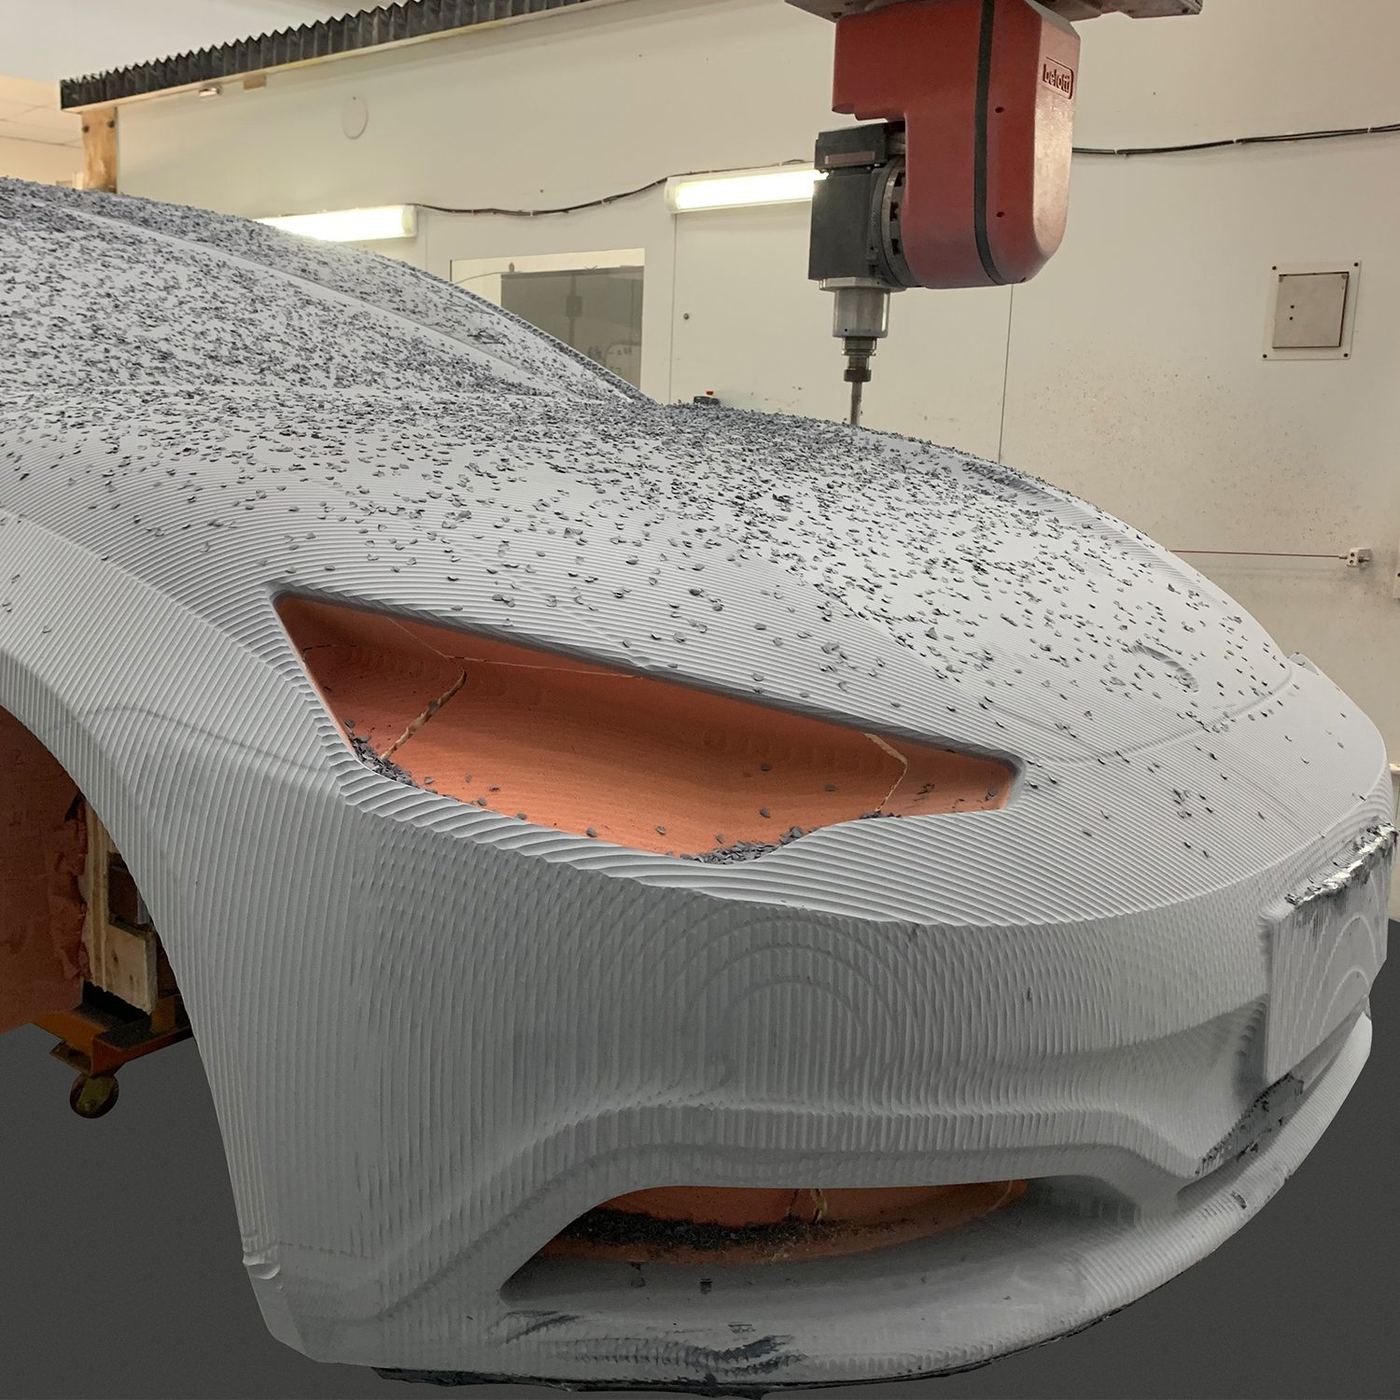
Five-axis gantry mill, 24,000 rpm, working envelope 8 × 4.2 × 2.5 m for full-size frames and buck work.
All six processes are quoted and inspected by the same Everoyal team, and parts from different lines consolidate into one shipment. See how a programme runs.
| Part | Usually | Why |
|---|---|---|
| Load-bearing joint housing, ±0.02 mm | CNC machining | Material is production-equivalent and the tolerance holds on a CMM |
| Cosmetic shell, 20–200 pcs, colour matched | Vacuum casting | Tooling cost stays near zero at that volume |
| Internal bracket with channels | Metal 3D printing | Geometry a cutter cannot reach |
| Flat panels and enclosure frame | Sheet metal | Bending and welding beat machining on weight and cost |
| Same cover at a few thousand | Rapid tooling + moulding | Per-part cost falls once the mould is paid for |
Rocky Chen replies with a process route, the tolerance risks we see in your data and a quotation — usually within one working day.