
Large Part Machining
A five-axis gantry mill with an 8 x 4.2 x 2.5 m envelope at 24,000 rpm, for frames and shells that will not fit a vertical centre. Large work is measured on a gantry CMM before it ships.
Gantry capability
8 × 4.2 × 2.5 m
Working envelope of the Italian five-axis gantry mill, large enough for a full body shell without splitting it.
24,000 rpm
Spindle speed on the gantry, high enough to finish large aluminum surfaces on the machine.
Gantry CMM
Full-size frames and whole assemblies are measured on the gantry CMM rather than a bench machine.
0.02 / 0.01 mm
Positional tolerance held to 0.02 mm across the part, precision bores to 0.01 mm.
Large parts fail in two ways. They do not fit, or they fit and move when the last clamp comes off. The gantry answers the first question. The second is a fixturing and inspection question, and it is settled before any cutting starts.
A vertical machining centre travels 2 x 1.2 x 0.9 m. Past that, the usual answer is to split the part into sections and weld or bolt them back together, which adds a tolerance stack at every seam and a distortion risk at every weld. The gantry removes the seam: a full-size frame or body shell is cut from one programme, against one datum.
The work that lands here is structural. Full-size robot frames, body shells, foam body models and the checking fixtures that have to match the part they measure.
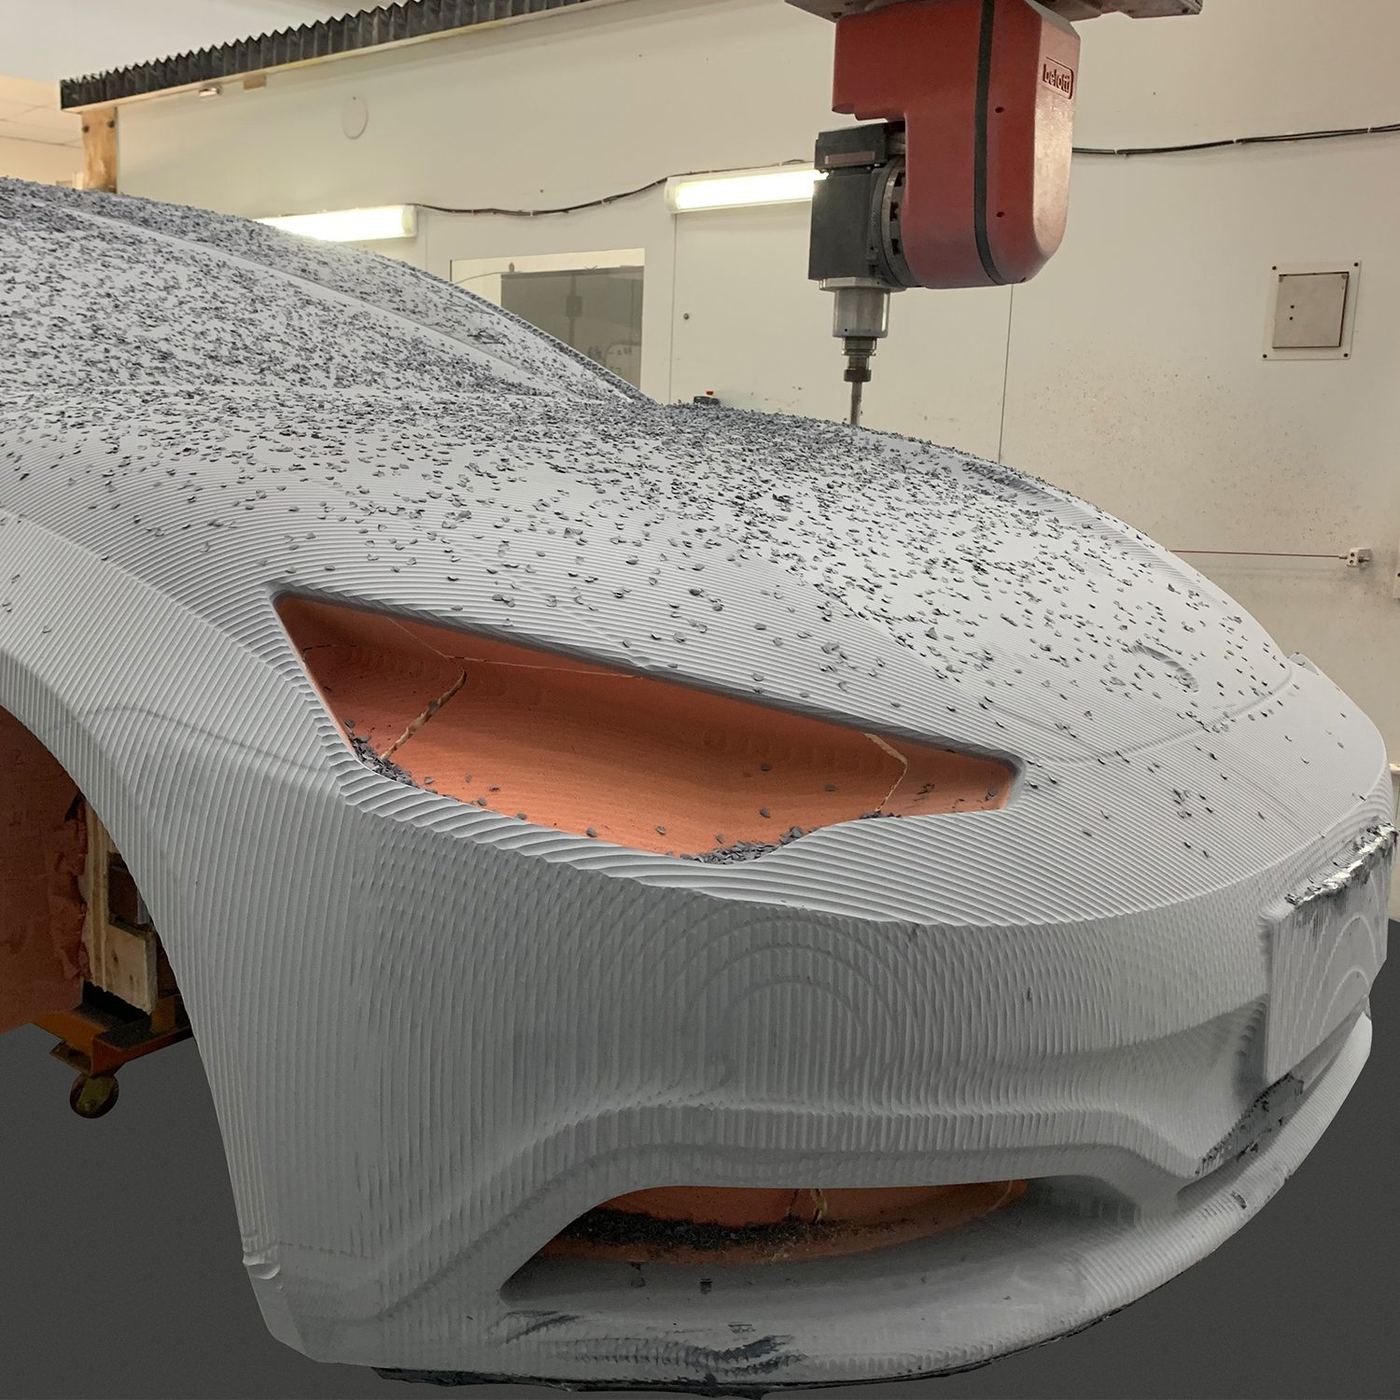 Large foam body shell on the gantry
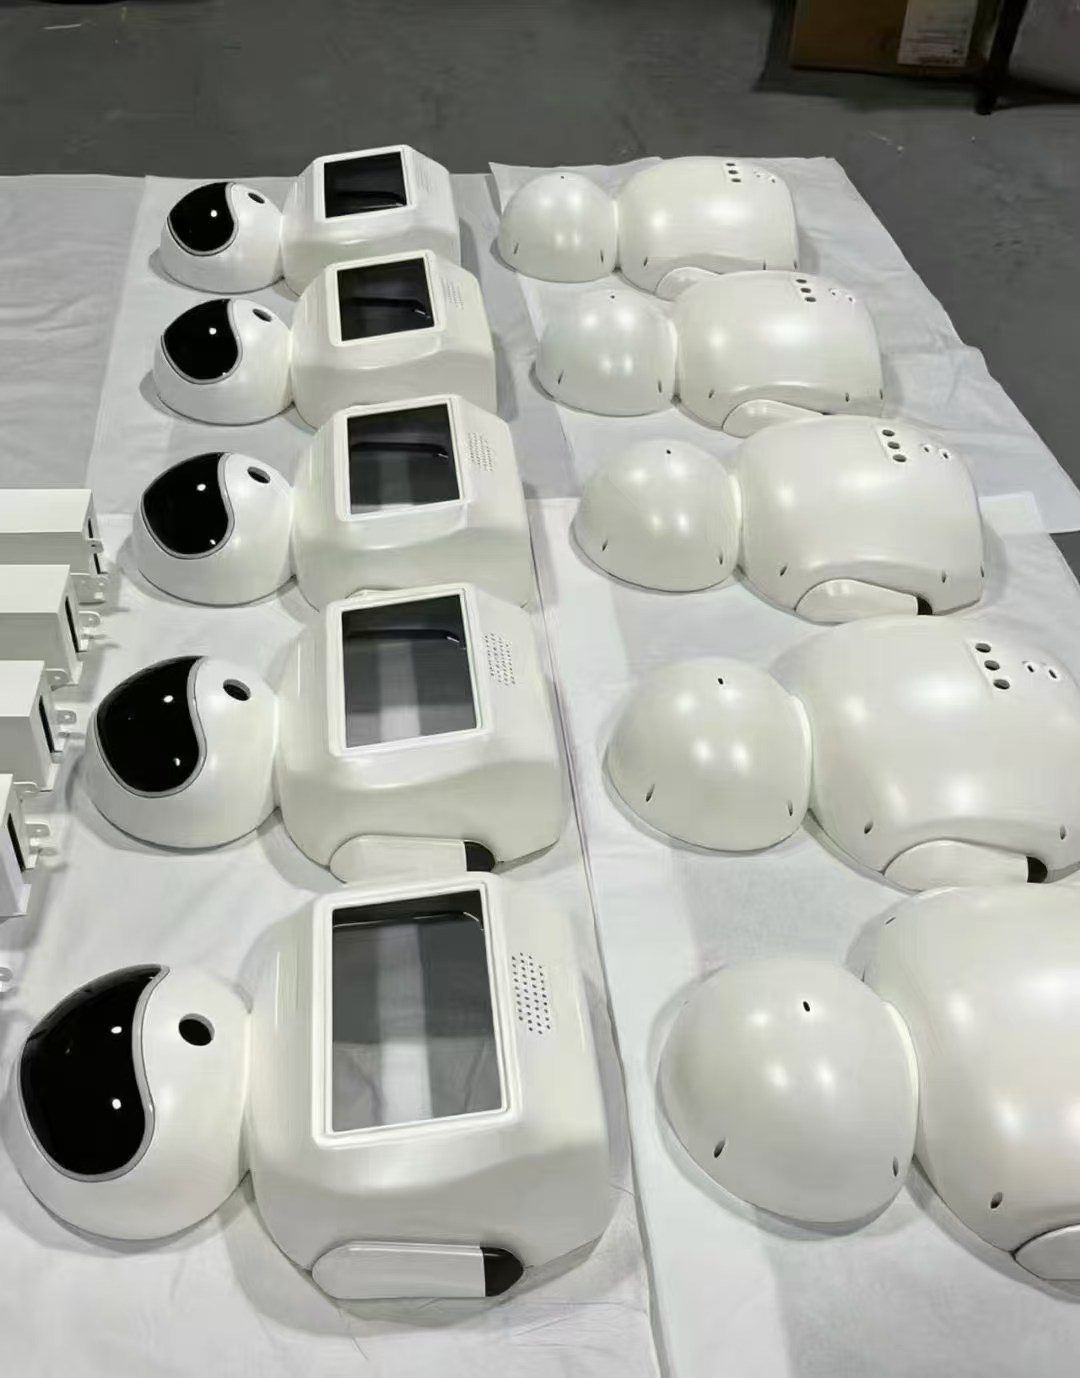 Head and body batches awaiting assembly
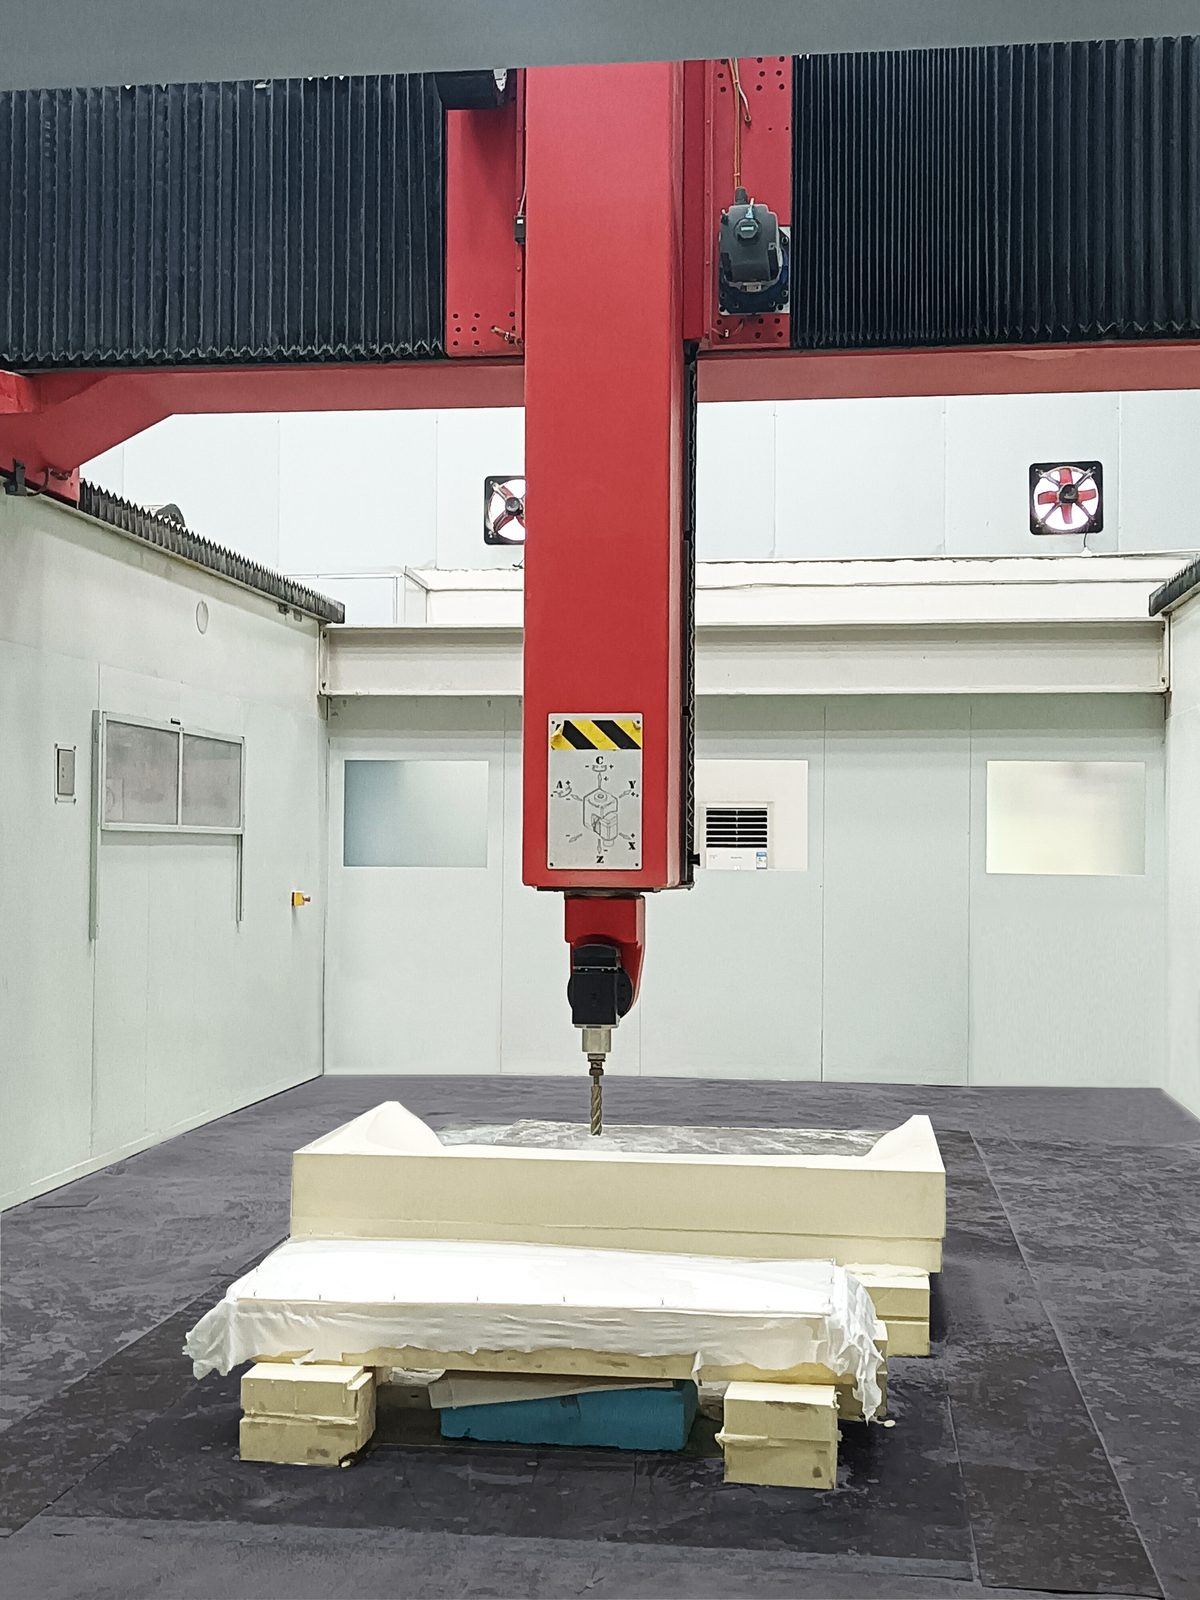 Italian-imported five-axis gantry machining center
 Five-axis machining bay
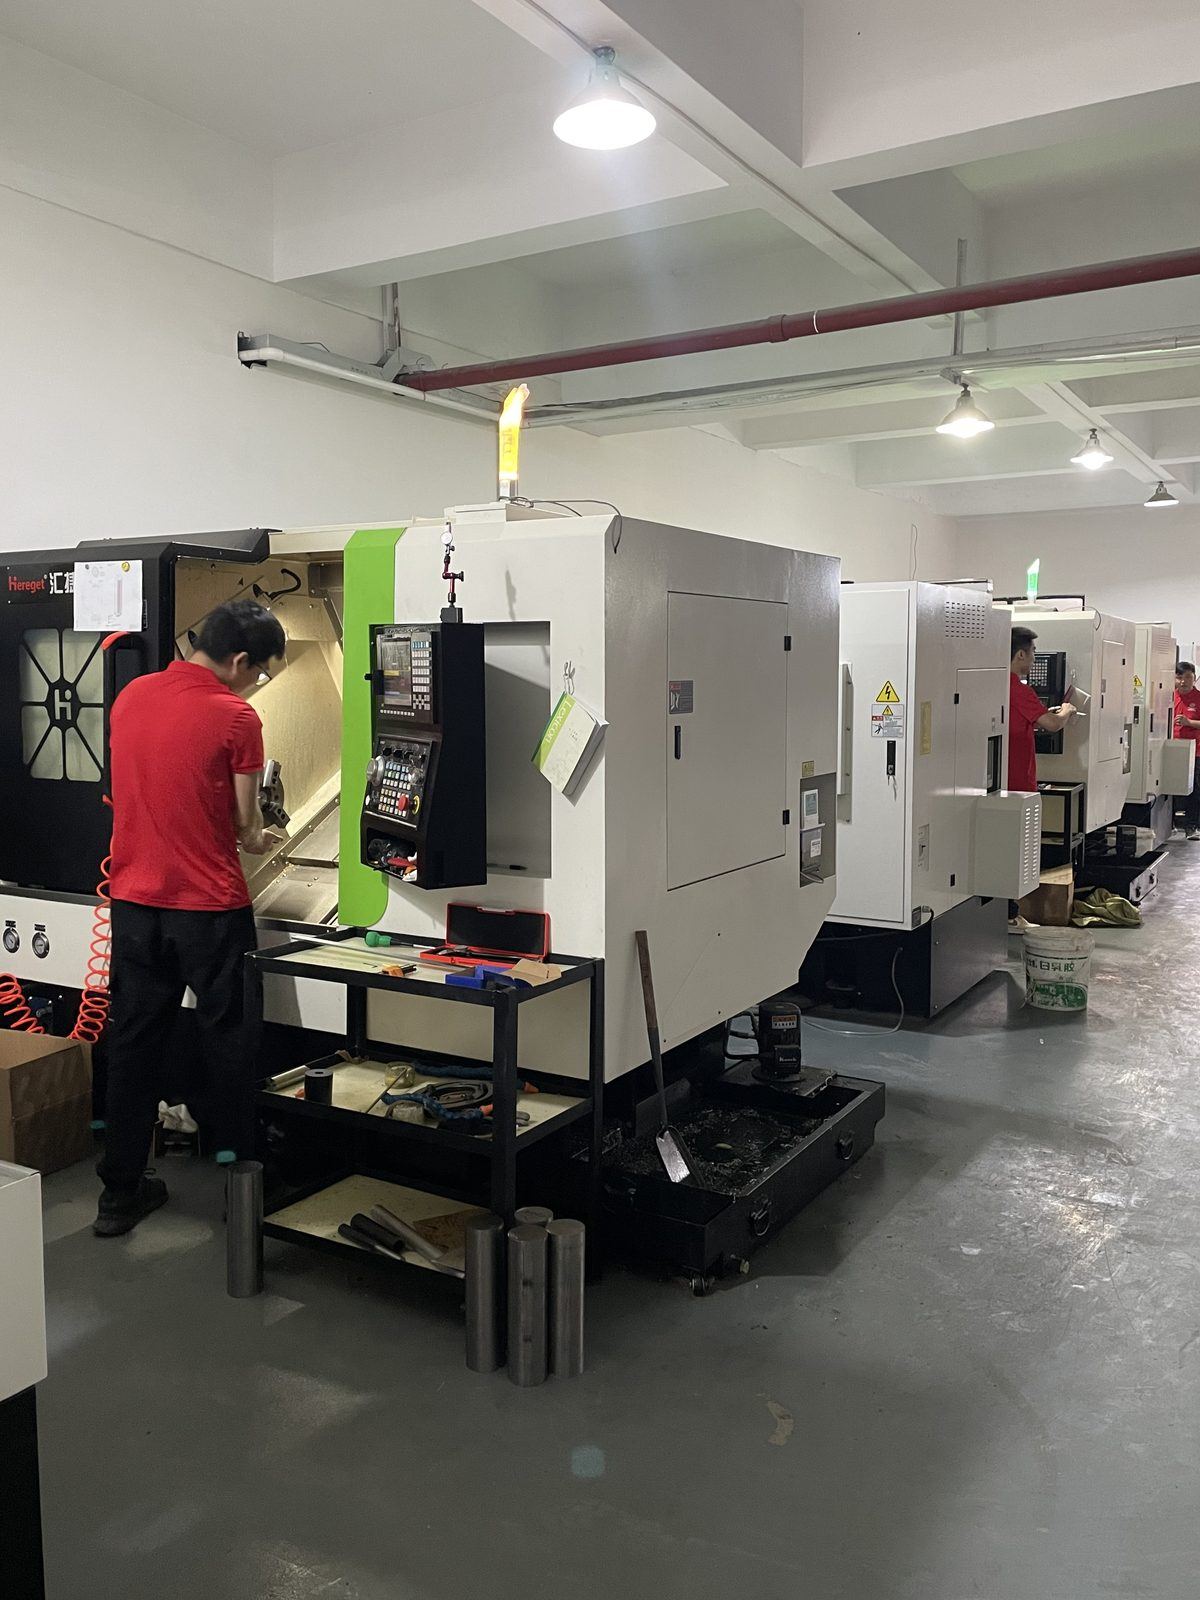
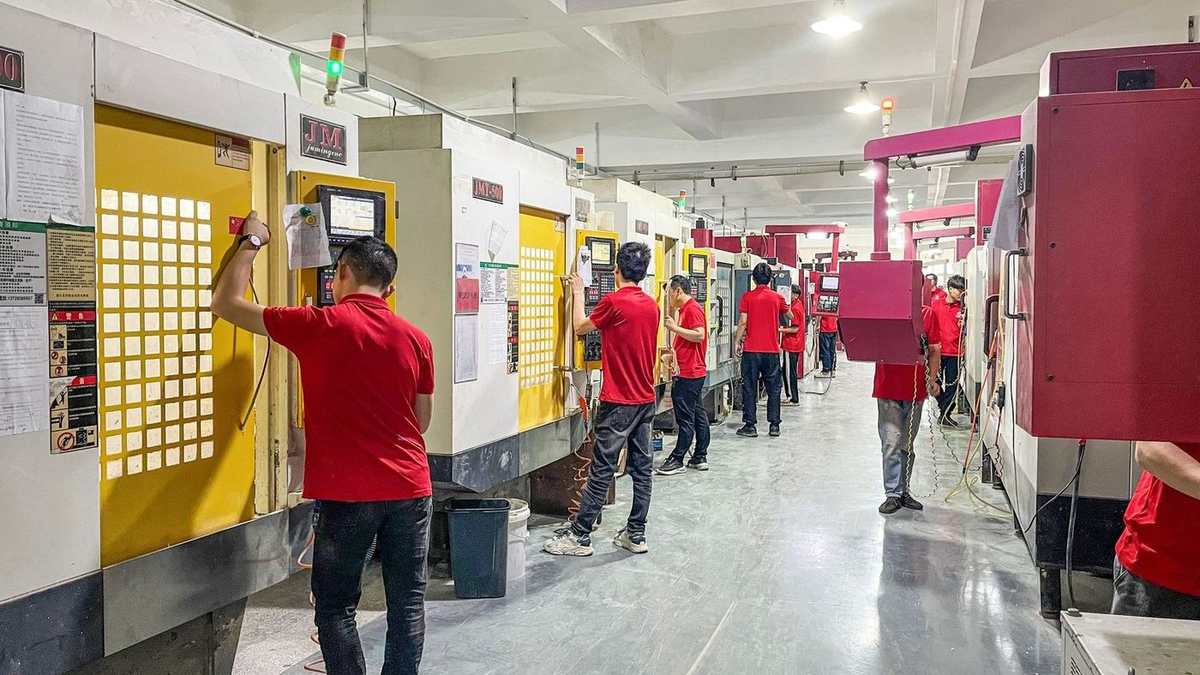 Operators at the vertical machining centers
Where a part goes, and why
Size is the first filter, but not the only one. A part that fits a vertical centre and still needs five faces cut in one set-up belongs on a machine that can reach all of them without re-fixturing.
| Machine | Envelope | What it takes |
|---|---|---|
| Vertical machining centre | 2 × 1.2 × 0.9 m | Part models, housings and small batches, up to 35,000 rpm |
| Five-axis gantry mill | 8 × 4.2 × 2.5 m | Full-size frames, body shells and assemblies that would otherwise be split, at 24,000 rpm |
Where a part sits between the two, the DFM review decides on geometry rather than on convenience. A frame that fits the vertical centre but carries bores on opposite faces is still a gantry job if re-fixturing would move the datum.
What a seam costs
Every seam is a tolerance stack
Two halves each held to 0.02 mm can still miss each other at the joint. What the customer measures is the stack, not either half.
Welding moves the datum
Heat pulls a welded frame away from the machined reference. The post-weld machining pass is where that cost appears.
One programme, one record
A part cut in one set-up carries one program sheet, one fixture record and one CMM report, which is what a traceable build needs.
Full detail on the prototype workflow page.
What the drawing can ask for
| Requirement | What is held | Where it applies |
|---|---|---|
| Positional tolerance | 0.02 mm | Mating faces, bore positions, register features |
| Precision bore | 0.01 mm | Bearing and joint bores measured before the part leaves the bay |
| General capability | 0.1 to 0.3 mm | Process dependent, stated on the drawing |
| Below 0.05 mm | Stays machined | Features that cannot be cast to tolerance |
| Geometric tolerance | ISO 1101 or ASME Y14.5 equivalent | Flatness, parallelism, position |
| Unspecified tolerance | ISO 2768 general table | Where the drawing gives no individual value |
| Machined surfaces | ISO 1302 roughness grades | Sealing and sliding faces |
Inspection follows the part, not the batch size. Prototypes and machined parts are checked 100% on a Zeiss CMM and a ROMER measuring arm, and the report ships with the parts. Batch production runs on 5% random sampling at an agreed depth.
How large a part can Everoyal machine?
The Italian five-axis gantry mill has an envelope of 8 x 4.2 x 2.5 m and runs at 24,000 rpm. Parts past the 2 x 1.2 x 0.9 m travel of the vertical centres go to the gantry instead of being split.
How is a large machined part measured?
Full-size frames and whole assemblies are measured on the gantry CMM. Prototypes and machined parts are inspected 100% on a Zeiss CMM and a ROMER arm, and the CMM report ships with the parts. Batch production uses 5% random sampling at an agreed depth.
What tolerance can a large part hold?
Positional tolerance is held to 0.02 mm and precision bores to 0.01 mm. General capability is 0.1 to 0.3 mm depending on the process, and any feature that needs to be below 0.05 mm stays on the machining route.
Can a full robot body be cut in one set-up?
If the part fits the 8 x 4.2 x 2.5 m envelope, it can be cut in one programme. Where the geometry forces a split, the DFM review sets the split line and a datum on each half before cutting starts.
Do you machine foam models and checking fixtures?
Yes. Large foam body shells are machined on the gantry. Checking fixtures used in metrology are kept with the program record, so a repeat order re-uses the same set-up.
Is there a minimum order for a large part?
One piece. The same inspection chain runs for a single prototype and for a batch, and only the sampling depth changes between them.
Overseas buyers RFQ: large part machining China. Smaller machined parts and turning-milling work: CNC machining. Fixtures and metrology: facilities. Inspection sequence: quality system.
Design notes for large enclosures are in the machine enclosure design guide.
Send the drawings, get a DFM view back
Rocky Chen replies with a process route, the tolerance risks we see in your data and a quotation — usually within one working day.